

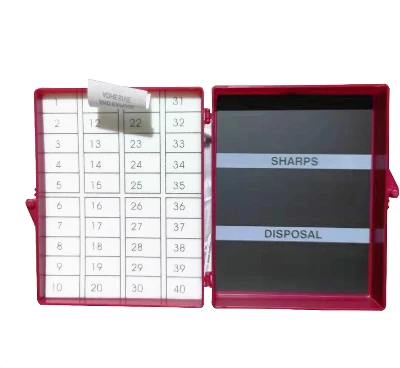
A surgical needle counter box is an essential medical consumable used in operating rooms to ensure accurate tracking of surgical needles and sharps during procedures. According to Wikipedia's entry on surgical safety, one of the most critical aspects of surgery is maintaining strict control of all instruments and sharps to prevent retention inside the patient. Needle counter boxes play a vital role in this process by providing a secure way to store and count needles during surgery.
For hospital procurement teams, distributors, and OEM brands, understanding the manufacturing process of surgical needle counter boxes helps in evaluating product quality and selecting reliable suppliers. Below is an overview of how these products are made in certified medical consumables factories.
1. Raw Material Selection
Production begins with medical-grade plastics such as polypropylene (PP) or ABS for the box shell, and high-density medical foam for the insert. The foam allows used needles to be safely locked in place, reducing the risk of sharps injury. Reputable factories in China ensure all raw materials are non-toxic, latex-free, and compliant with ISO 13485 and CE standards.
2. Injection Molding of the Plastic Shell
The outer case of the needle counter box is produced using injection molding technology. Precision molds ensure uniform size, smooth edges, and durability. Some OEM surgical consumables suppliers also allow custom branding or color-coding for hospitals and distributors.
3. Foam Insert Fabrication
The foam insert is cut and shaped to fit the box interior. Each piece is designed with pre-cut slots or grids, allowing surgical staff to secure and count needles easily during procedures. The foam must have strong absorption and puncture resistance, ensuring safe disposal after use.

4. Assembly and Sterile Packaging
After molding and foam cutting, the two components are assembled manually or by semi-automated lines. The assembled boxes are then packed in sterile packaging to prevent contamination. Most bulk needle counter boxes from China factories are sealed in medical-grade pouches, with optional OEM private labeling available for international distributors.
5. Quality Control and Certification
Before shipment, every batch undergoes strict quality inspection, including:
Sharp retention test (ensuring needles remain securely fixed in foam)
Structural durability test (resistance to breakage during use)
Sterility validation
Only products that pass these checks are shipped. Certified manufacturers provide documentation such as ISO 13485, CE marking, and FDA registration for international compliance.

Why This Matters for B2B Buyers?
For hospital purchasing managers, distributors, and medical wholesalers, choosing the right supplier for surgical needle counter boxes means ensuring:
Consistent quality across large-scale orders
Compliance with international standards
Flexible OEM customization options
Reliable lead times from high-capacity factories
Bulk procurement from an experienced medical consumables manufacturer in China ensures cost efficiency without compromising safety.